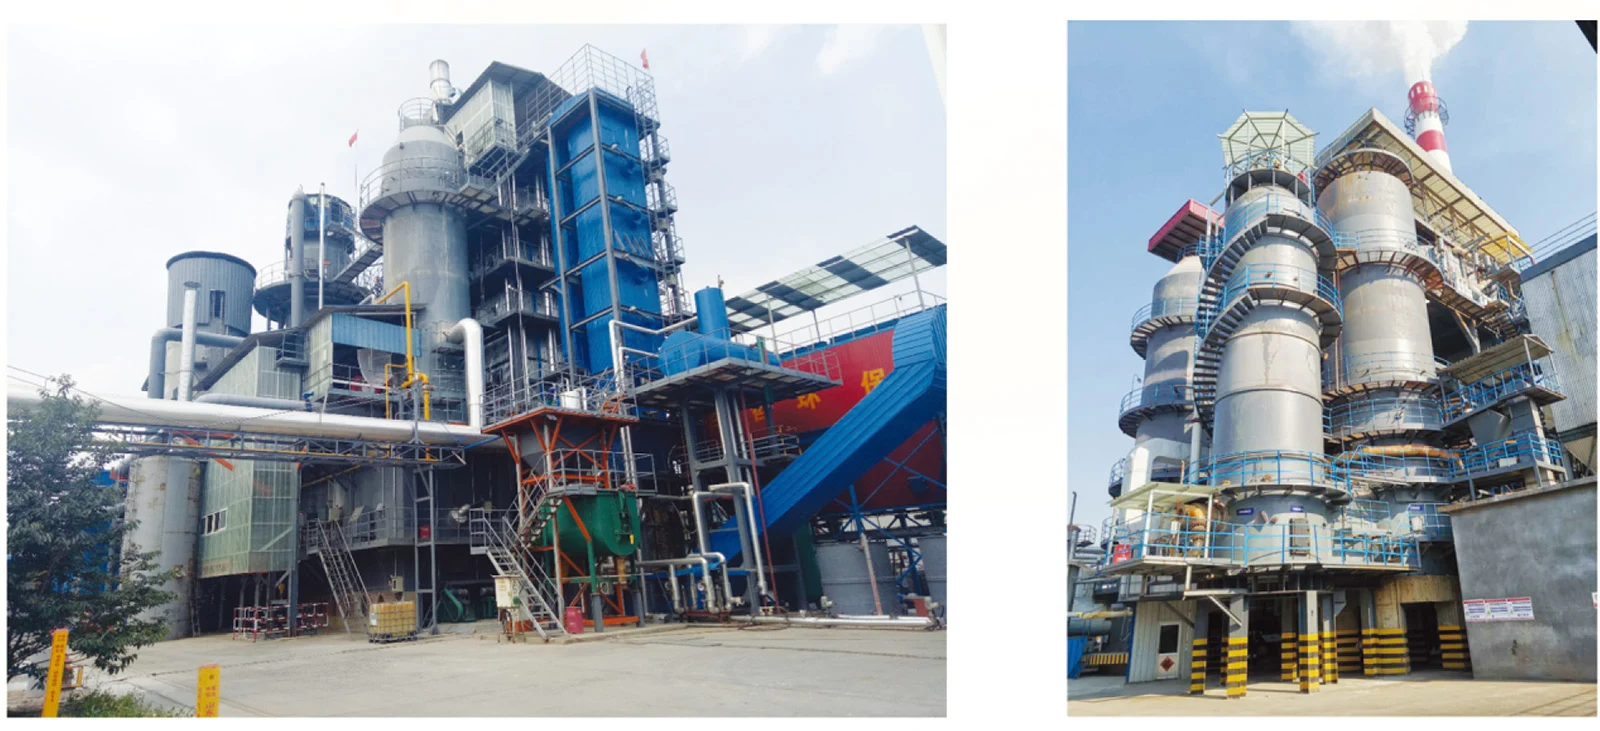
Integrated thermal treatment and heat recovery systems for suitable industrial waste liquids, gases and solids. Each project starts with the waste characteristics, required treatment rate and intended steam use.
PLAN YOUR BOILER PROJECT
What we need to specify your system
- Waste composition and physical form, with available analysis
- Treatment rate, operating hours and supporting fuel
- Steam requirements, site conditions and applicable local requirements
Incinerator and system for high temperatureharmless treatmentof "three wastes in industry
—
Technical advantages and characteristics
1. The use of high-efficiency co-combustion fumace technology, high pollution, difficult to degradeand toxic waste water, waste gas, waste and other fuels at the same time into High-temperature incinera-tion, set buming, efficient combustion, pyrolysis as a whole, completely overcome the combustion is notcomplete, environmental pollution is not up to standard technology problem.
2. The incinerator and the heat recovery furnace into a furnace, to achieve the integration, integra-tion, compact structure, reduce land area, Save investment.
3. Incineration furnace with a special vertical, closed structure, to achieve continuous gray andlong system operation, to improve the burning rate.
4. Load regulation characteristics, and can be stable in the range of 30% 100% rated load, toachieve the effect of economic operation;
5. The incinerator has the advantages of high automation, high combustion stability, high safetyand convenient operation and maintenance.
Application scope
Production of toxic waste water, waste residue, waste gas produced in the petrochemicalindustry or can not be handled by general biochemical methods Waste water, waste residue,exhaust gas, only the use of high temperature incineration method. Experience to introducethe above waste at 1000 °C under the conditions of stay Between> 2S can be decomposedinto harmless emissions, can be considered denitrification, desulfurization, dust.